Thank you for writing to us. One of our executive will reach back to you through your submitted medium. In case there’s an urgency, feel free to connect over WhatsApp for faster response.
Prefer calling? Dial +918048032976 (International callers) or 08048032976 (Indian callers).
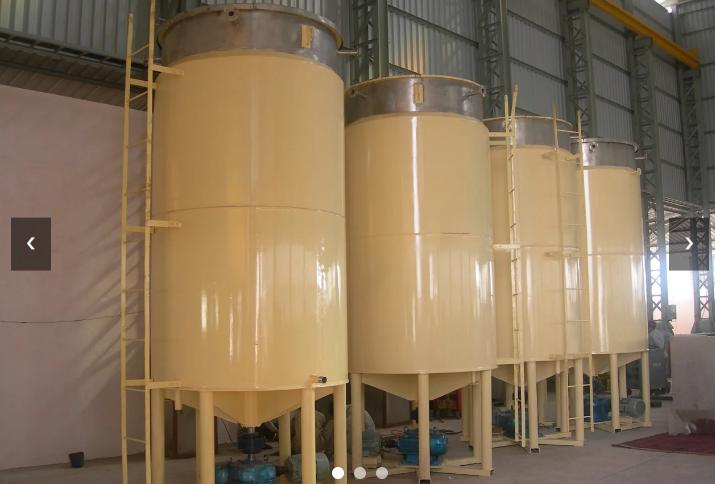
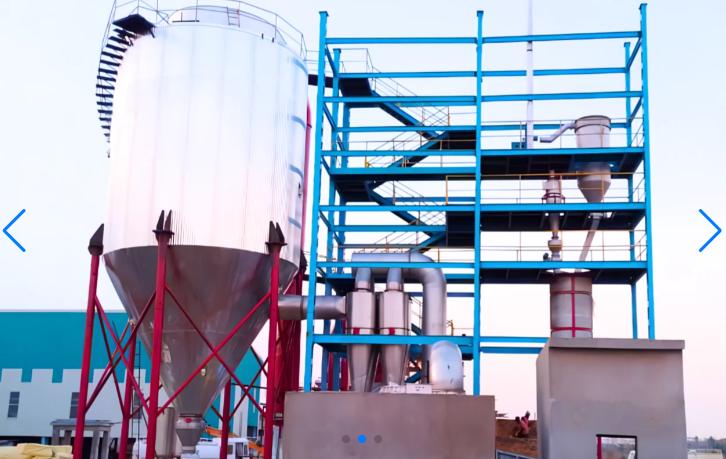
A silo is a specialized structure for storing bulk materials such as grain, coal, cement, carbon black, wood chips, and food products. Storage silos are essential equipment in manufacturing, agriculture, mining, and food processing industries.
Raj Process is a leading manufacturer of storage silos in India, offering durable and efficient designs tailored to meet the specific needs of diverse industries. Built with high quality materials and advanced manufacturing techniques, our silos are engineered to withstand harsh industrial environments while ensuring product safety and quality.
Storage Silo Solutions
Raj Process silos are designed to prevent contamination and maintain product integrity. With expertise in spray drying and powder handling, we also provide advanced egg powder production plants capable of drying whole egg, yolk, and albumen. To ensure optimal product quality, separate dryers are recommended for each product type.
Typical Applications
Foodstuffs and flour silos
Chemical silos
Coal silos
Cement and fly ash silos
Grain silos
Ceramic powder silos
Features
Available in bolted, smooth wall, and welded designs
Material options: epoxy coated carbon steel, stainless steel, carbon steel with stainless steel cladding, carbon steel with FRP coating
Designed for durability and safe operation under demanding conditions
Customizable to integrate seamlessly into existing process setups
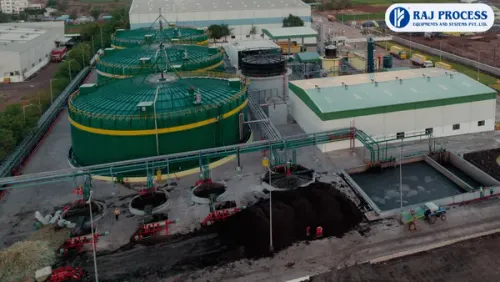
Raj Process Equipments & Systems Pvt. Ltd. is a pioneer in compressed biogas (CBG) technology, offering patented solutions for biogas generation and purification. As one of India’s leading CBG plant manufacturers, we deliver turnkey systems that convert organic waste into high purity compressed biogas — a sustainable, eco friendly fuel for the future.
Aligned with national initiatives like SATAT and GOBARdhan, Raj Process is driving India’s clean energy transition by designing and executing next generation CBG plants across the country and globally.
Organic Waste In. Clean Fuel and Fertilizer Out.
Compressed Biogas — commonly called Bio-CNG — is biomethane produced from the anaerobic digestion of organic waste, purified to 96–99% methane purity, and compressed to 200–250 bar for dispensing and sale. It is chemically identical to fossil CNG in energy value, calorific content, and physical properties. Every CNG vehicle on the road can run on CBG without any modification. Every existing CNG dispensing station is compatible.
The process, in simple terms:
Organic waste enters a sealed, temperature-controlled digester. Over 15–25 days, a carefully managed consortium of microorganisms breaks it down and produces raw biogas — typically 55–65% methane and 35–40% CO₂. This raw biogas passes through our cleaning and upgrading systems, where CO₂, hydrogen sulphide, moisture, and trace contaminants are removed. What remains is biomethane meeting IS 16087:2023 specifications. We compress it, store it in high-pressure cascade systems, and it is ready for sale to Oil Marketing Companies or direct consumers.
The digestate — the solid and liquid material remaining after digestion — is not waste. It is a nutrient-rich Fermented Organic Manure (FOM) and bio-slurry that sells as a premium organic fertilizer, adding a second revenue stream to your plant from day one.
One plant. One waste problem solved. Two revenue streams generated. That is the CBG business model.
FEEDSTOCKS
The feedstock landscape for CBG production in India is broad. We have designed and commissioned plants running on:
Napier grass and dedicated energy crops
Press mud from sugar mills
Cattle and cow dung
Distillery spent wash — molasses based and grain-based
Municipal solid waste (organic fraction)
Poultry litter
Food processing effluents
Fruit and vegetable market waste
Rice straw and wheat straw
Sugarcane trash and bagasse
Sewage sludge
Biogas yields across these feedstocks range from 30 m³ per tonne for cattle dung to 350–400 m³ per tonne for high-fat food waste. The differences are not just in yield — each feedstock brings its own pre-treatment requirements, C:N ratio considerations, sulphur loading, and digester design implications.
Premium Spray Drying Solutions: Engineering Excellence by Raj Process
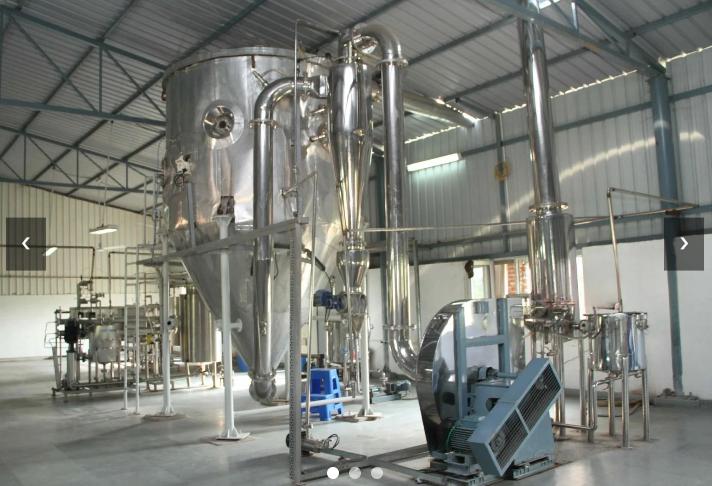
In the landscape of industrial thermal processing, Raj Process has solidified its reputation as the premier spray dryer manufacturer in India. Our systems represent the pinnacle of liquid-to-powder conversion technology, offering unparalleled efficiency for diverse industrial sectors.
The Science of Spray Drying: How It Works
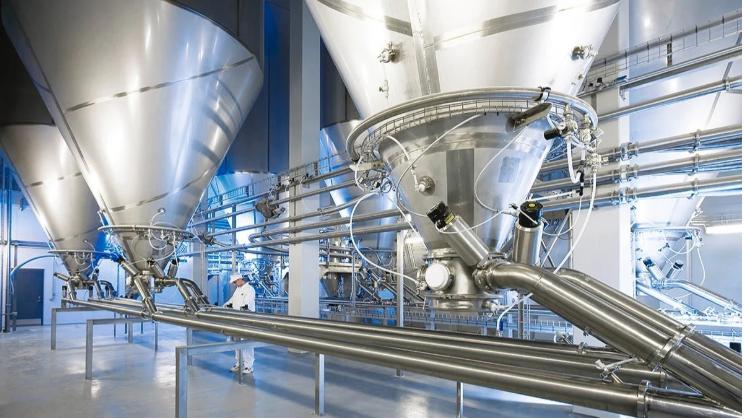
Spray drying is a sophisticated method of producing a dry powder from a liquid or slurry by rapidly drying with a hot gas. It is the preferred method for thermally sensitive materials because the drying process is near-instantaneous.
The process follows four fundamental stages:
Atomization: The liquid feed is turned into tiny droplets using a nozzle or rotary atomizer.
Spray-Air Contact: The droplets meet a stream of hot air.
Drying: Moisture evaporates instantly, cooling the particle as it dries.
Separation: The dry powder is recovered from the exhaust air using cyclones or bag filters.
Technical Specifications & Capacity
At Raj Process, we engineer systems that scale with your business. Whether you are in a R&D phase or high-volume industrial production, our equipment is built to perform.
Key Features of Raj Process Spray Dryers
1. Advanced CIP (Cleaning-In-Place) Systems
Hygiene is non-negotiable in pharmaceutical and food processing. Our integrated CIP systems provide:
Automated Cycles: Thorough cleaning without dismantling the machinery.
Cross-Contamination Prevention: Essential for facilities handling multiple product lines.
Reduced Downtime: Faster transitions between product batches.
2. Versatile Feed Handling
Our nozzles and atomizers are designed to handle various feed types:
Solutions: Clear liquids with dissolved solids.
Slurries: Thick, high-viscosity liquids with suspended solids.
Emulsions: Mixtures of immiscible liquids (like oil and water).
3. Precision Control
We utilize advanced PLC-based control systems to monitor inlet/outlet temperatures and feed rates, ensuring a consistent particle size distribution for every batch.
Industrial Applications: Where Precision Meets Scale
As leading manufacturers, we serve a massive spectrum of industries. Below is a detailed breakdown of how our spray dryers are utilized:
Food & Dairy
Milk Powder: Transforming fresh milk into shelf-stable powders while preserving nutritional value.
Fruit Pulps: Creating instant fruit powders for beverages and baking.
Flavors: Encapsulating volatile flavor oils to extend shelf life.
Pharmaceuticals & Biotechnology
Herbal Extracts: Processing sensitive botanicals into concentrated, easy-to-dose powders.
Enzymes: Gentle drying to maintain biological activity.
API Processing: Precise particle engineering for drug delivery.
Chemical & Mineral
Detergents: Large-scale production of uniform, free-flowing washing powders.
Ceramics & China Clay: Preparing fine powders for high-quality molding and glazing.
Dyestuffs: Ensuring consistent color strength and solubility.
Why Choose Raj Process?
Choosing the right spray dryer manufacturer in India is a long-term investment. Raj Process offers:
Custom Engineering: Every system is tailored to the specific thermal sensitivity and viscosity of your product.
Energy Efficiency: Optimized heat recovery systems to reduce operational costs.
Durability: High-grade stainless steel construction (SS316/SS304) for longevity and compliance.
High-Efficiency Rotary Dryer Solutions: The Ultimate Industrial Guide
In the modern industrial landscape, moisture control is the difference between a high-quality product and a wasted batch. As a premier Rotary Dryer Manufacturer, RAJ Process provides engineering marvels designed to handle the most challenging materials with precision, durability, and thermal efficiency.
Our rotary drying systems are engineered to transform wet cakes, powders, and minerals into high-value dry products. Whether you are processing silica sand or delicate coconut powder, our technology ensures uniform drying with minimal energy consumption.
1. What is a Rotary Dryer? (Technical Overview)
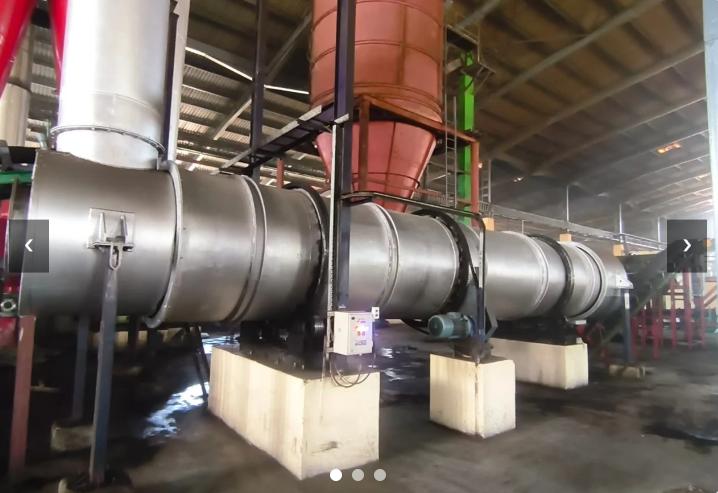
A Rotary Dryer is a type of industrial dryer employed to reduce or minimize the liquid moisture content of the material it is handling by bringing it into direct or indirect contact with a heated gas.
The dryer consists of a large, rotating cylindrical tube, usually supported by steel beams. The dryer slopes slightly so that the discharge end is lower than the material feed end in order to convey the material through the dryer under gravity.
How It Works: The Three-Step Process
Feeding & Distribution: Wet material is fed into the drum. Internal “flights“ (lifting blades) pick up the material and shower it through the hot air stream.
Heat Transfer: As the drum rotates, the material makes contact with heated gas. This can be done via Direct Firing (gas touches material) or Indirect Firing (heat transferred through the drum wall).
Moisture Evacuation: Vaporized moisture is carried away by the air stream and filtered through a cyclone or bag filter, while the dry product exits the lower end.
2. Industry-Leading Capacity & Performance
We design our systems to accommodate everything from boutique processing to massive mining operations.
3. Rotary Dryers vs. Calciners: Versatility Redefined
One of the key advantages of our engineering is the ability to use these units as Calciners.
Drying: Removes surface or bound moisture at lower temperatures.
Calcination: Involves heating the material to high temperatures (up to 600°C) to induce a chemical change or phase transition.
Because our drums are built with heat-resistant alloys, a RAJ Process Rotary Dryer can double as a calciner, making it a “two-in-one“ asset for chemical and mineral plants.
4. Strategic Advantages of Our Rotary Drying Systems
A. Material Versatility
Unlike flash dryers or spray dryers, rotary dryers are incredibly “forgiving.“ They can handle:
Sticky Cakes: Using specialized internal chain systems to prevent clogging.
Non-Uniform Sizes: From fine dust to large mineral chunks.
Abrasive Solids: Reinforced shells that withstand constant friction.
B. Energy Efficiency & Heat Recovery
We integrate advanced heat exchangers that pre-heat the incoming air using the exhaust gas, significantly lowering the “Cost Per Ton“ of dried product.
C. Customized Internal Flights
The “flights“ inside the drum are the secret to efficiency. We customize flight patterns (radial, cruciform, or honeycomb) based on your material’s flow characteristics to ensure a perfect “curtain“ of material for maximum heat exposure.
5. Extensive Industrial Applications
Our rotary dryers are deployed across diverse sectors. Here is how we add value to specific materials:
Mineral & Construction Industry
Silica Sand: Essential for glass and foundry industries. We provide high-temp drying to ensure 0.1% moisture content.
Limestone & Gypsum: High-capacity drying for cement and wallboard production.
China Clay: Precise temperature control to prevent discoloration.
Agriculture & Food Processing
Coconut Powder: Gentle drying at controlled temperatures to preserve natural oils and flavor.
Bagasse: Converting sugar mill waste into high-calorie biofuel by reducing moisture for better combustion.
Grain & Seed: Large-scale moisture reduction for long-term storage.
Chemical & Waste Management
Sludge Drying: Reducing the volume of industrial sludge for cost-effective disposal.
Fertilizers: Creating free-flowing granules that don't cake during packaging.
6. Engineering & Maintenance: Built for Longevity
As a leading manufacturer, we don't just sell equipment; we provide a lifecycle solution.
Precision Alignment: Our technicians use laser alignment for the trunnion rollers to ensure the drum rotates with minimal vibration, extending the life of the bearings.
Sealing Technology: Advanced graphite or mechanical seals prevent dust leakage and maintain thermal vacuum.
Automation: Fully integrated PLC panels allow for remote monitoring of moisture levels and fuel consumption.
In the modern era of “Zero Liquid Discharge“ (ZLD) and high-purity chemical processing, the demand for efficient thermal separation has never been higher. As a premier Agitated Thin Film Dryer (ATFD) Manufacturer, RAJ Process delivers cutting-edge evaporation solutions engineered to handle the most complex, heat-sensitive, and high-viscosity fluids.
Our systems are designed to maximize heat transfer, minimize residence time, and ensure that even the most difficult-to-handle slurries are converted into high-quality solids or concentrated liquids.
1. Understanding ATFD Technology: The Science of Thin Films
An Agitated Thin Film Dryer (ATFD) is a vertical or horizontal thermal separation unit. Unlike traditional evaporators where the liquid sits in a vessel or flows through tubes, the ATFD uses mechanical agitation to create a highly turbulent, thin film of product against a heated jacketed wall.
How the Process Works
Feed Entry: The liquid or slurry enters the top of the cylindrical heating jacket.
Thin Film Formation: A high-speed rotor with specialized blades spreads the liquid into a thin film (typically 0.5 to 2 mm thick) across the internal heated surface.
Rapid Evaporation: Because the film is so thin, the heat transfer is near-instantaneous. Vapors travel upward through a mist eliminator.
Solid Recovery: As the moisture evaporates, the material transitions from a liquid to a paste, and finally into a dry powder or flakes, which are discharged at the bottom.
2. Technical Specifications & Performance Chart
Our ATFD units are custom-built to match the thermal sensitivity of your specific product. Below is the standard technical roadmap for our high-performance systems.
3. Specialized Rotor Blade Configurations
The “heart“ of an ATFD is its rotor. Depending on whether your material is sticky, abrasive, or heat-sensitive, we offer four distinct blade configurations to optimize your yield:
A. Fixed Blade Rotor
Best For: Low to medium viscosity liquids.
Mechanism: Maintains a precise, fixed clearance between the blade tip and the heated wall. It is ideal for continuous, high-speed evaporation of stable solutions.
B. Cylindrical Wiper Rotor
Best For: Highly viscous fluids and concentration tasks.
Mechanism: Uses wipers to physically “wipe“ the film across the surface, preventing any stagnant “hot spots“ that could degrade the product.
C. Spring-Loaded Rotor
Best For: Products that tend to scale or form a hard crust on the walls.
Mechanism: The blades are pushed against the wall by spring tension, ensuring the heating surface stays clean and heat transfer remains at 100% efficiency throughout the run.
D. Centrifugal Blade Rotor
Best For: Slurries with high solids content.
Mechanism: Utilizes centrifugal force to press the blades outward. As the product thickens, the blades adapt to the changing resistance, making it the most versatile option for multi-product plants.
4. Key Advantages of Using ATFD Systems
Zero Liquid Discharge (ZLD) Compliance
In today’s regulatory environment, industrial plants are under pressure to eliminate wastewater. Our ATFDs act as the final stage of a ZLD plant, taking the “reject“ from Reverse Osmosis (RO) or Multi-Effect Evaporators (MEE) and turning it into dry, disposable salt or reusable solids.
Minimal Residence Time
Traditional evaporators can subject a product to heat for hours. In an ATFD, the residence time is measured in seconds. This is critical for pharmaceuticals, flavors, and enzymes that would otherwise lose their potency or change color if exposed to heat for too long.
Single-Pass Operation
Our technology allows for a “liquid-in, powder-out“ transition in a single pass. This eliminates the need for separate thickeners, centrifuges, or secondary dryers, significantly reducing your plant's footprint and capital expenditure.
5. Industrial Applications Across Sectors
Pharmaceutical & Biotech
Concentrating APIs: Gentle handling of active pharmaceutical ingredients.
Solvent Recovery: Efficiently separating high-value solvents from waste streams.
Herbal Extracts: Maintaining the bio-activity of natural extracts during concentration.
Chemical & Petrochemical
Dye & Pigment Concentration: Achieving high-purity colorants.
Agrochemicals: Drying pesticides and fertilizers into stable powder forms.
Resin Processing: Handling high-viscosity polymers without clogging.
Food & Beverage
Dairy Products: Concentrating whey and milk derivatives.
Fruit Pulps: Reducing volume for transport while preserving nutritional integrity.
Sweeteners: Processing sugar alcohols and corn syrup.
6. Engineering Excellence: Why RAJ Process?
Choosing the right ATFD manufacturer is about more than just buying a machine; it’s about process reliability. We provide:
Custom Simulation: We use thermal modeling to calculate the exact surface area required for your specific mass balance.
Integrated Milk Powder & Condensed Milk Processing Solutions
In the rapidly evolving dairy industry, the ability to convert raw milk into high-value, shelf-stable derivatives is the cornerstone of profitability. Raj Process Equipment stands at the forefront of this transformation, providing world-class Milk Powder Plants and Sweetened Condensed Milk (SCM) lines.
Feature, Specification
Processing Capacity, “500 LPH to 50,000 LPH“
Material of Construction- SS304 / SS316 / SS316L
Automation Level - Semi-Automatic to Fully Automatic (SCADA)
Evaporation System- Multi-Effect Falling Film Evaporator
Drying System,High- Pressure Spray Dryer with Fluid Bed
Packing Options- “Tins, Barrels, or Bulk Industrial Pouches“
Our engineering philosophy combines sterile construction with high-efficiency thermal dynamics, ensuring that your dairy products maintain their nutritional integrity while achieving maximum shelf life.
The Science of Sweetened Condensed Milk (SCM)
Sweetened Condensed Milk is more than just concentrated milk; it is a precisely engineered dairy product where sugar acts as the primary preservative. Through a process of controlled evaporation and osmotic pressure management, we create a product that is resistant to microbial spoilage.
Advanced Features of Raj Process Dairy Plants
At Raj Process Equipment, we prioritize “Total Cost of Ownership.“ Our plants are designed to be energy-efficient, easy to maintain, and fully compliant with global food safety standards.
1. Sterile Construction & Hygiene
Every pipe, valve, and vessel is constructed from high-grade stainless steel (SS316L/SS304) with a complete sanitary design. Our integrated Cleaning-In-Place (CIP) systems ensure that the entire production line is sterilized automatically, reducing manual labor and eliminating the risk of human error.
2. Automation: PLC & SCADA Integration
Modern dairy processing requires millisecond precision. Our plants are operated via a PLC-controlled SCADA system, providing:
Real-time Monitoring: Track temperatures, flow rates, and sugar brix levels from a central console.
Data Logging: Maintain digital records for quality audits and regulatory compliance.
Batch Consistency: Ensure every tin of condensed milk has the exact same texture and sweetness profile.
3. Thermal Efficiency
Milk is heat-sensitive. Our evaporators utilize Falling Film technology with multiple effects, allowing for high evaporation rates at lower temperatures. This prevents the “cooked“ flavor and browning (Maillard reaction) often found in lower-quality processing plants.
Diverse Industrial Applications
Raj Process Equipment designs versatile systems that can be adapted for a wide variety of dairy and non-dairy applications:
Dairy Sector
Whole Milk & Skim Milk Powder: Producing free-flowing, instantly soluble powders.
Infant Formula: Specialized lines requiring ultra-high hygiene and nutrient fortification.
Dairy Whiteners: Formulating powders with optimized fat-to-protein ratios for the beverage industry.
Industrial Food Processing
Bakery & Confectionery: Our SCM lines provide the bulk ingredient for chocolates, toffees, and premium baked goods.
Why Choose Raj Process Equipment?
Space-Optimal Engineering
We understand that floor space is a premium. Our engineering team specializes in vertical plant layouts that offer maximum throughput with a minimal physical footprint, allowing you to scale your production without needing massive land acquisitions.
Global Material Standards
We don't compromise on hardware. From the pumps to the sensors, every component is sourced from high-class, globally recognized manufacturers. This ensures that your plant operates with high uptime and minimal spare part requirements.
Turnkey Project Management
From the initial feasibility study and site layout to the final commissioning and staff training, Raj Process Equipment provides a true turnkey experience. Our expertise as a manufacturer in major industrial hubs allows us to provide rapid on-site support across the nation.
Ice Cream Manufacturing: Utilizing condensed milk for creamy texture and structural stability.
Innovation Spotlight: Compressed Biogas (CBG) Integration
In line with global sustainability trends, Raj Process Equipment is also a leading Compressed Biogas Manufacturer. We offer a unique circular economy model for dairy farms:
Waste to Energy: Convert cattle manure and dairy effluent into high-purity methane.
Plant Power: Use the generated Biogas to fire the boilers for your Milk Powder Plant.
Cost Reduction: Dramatically lower the carbon footprint and operational costs of your dairy processing facility.
In the evolving landscape of industrial bioprocessing, starch and its derivatives serve as the backbone for countless sectors—from biodegradable packaging to life-saving pharmaceuticals. Raj Process Equipment is a premier manufacturer and global leader in providing Turnkey Starch and Liquid Glucose Plants.
We don't just build machines; we engineer high-yield ecosystems. With decades of expertise and five world-class manufacturing units, we deliver custom-designed plants that process maize, cassava, potato, wheat, and rice into high-purity native starch, modified starch, and liquid glucose.
1. The Science of Starch: Extraction and Molecular Engineering
Starch is a natural glucose polymer stored in plant granules ranging from 1 to 140 µm. The challenge for any manufacturer is the efficient separation of this starch from fiber, protein, and gluten without damaging the granule structure.
Our Multi-Feedstock Capability
Our plants are engineered with the flexibility to handle diverse raw materials, ensuring your facility remains profitable regardless of seasonal crop fluctuations:
Maize (Corn): High-yield wet milling for starch and valuable by-products like gluten and germ oil.
Cassava/Tapioca: Specialized washing and peeling lines for high-viscosity starch extraction.
Potato: Cold-process extraction to maintain delicate granule integrity.
Rice & Wheat: Advanced separation techniques to manage high protein (gluten) content.
Native Starch Manufacturing Plants: Precision Extraction
Native starch is the raw, unmodified form used in bulk industries. Our process focuses on mechanical separation efficiency and water conservation.
Key Processing Stages:
Cleaning & Milling: Multi-stage cleaning removes impurities before high-speed milling breaks the cellular structure.
Fiber Separation: Utilizing high-capacity centrifugal screens to isolate starch milk from fibrous husks.
Hydrocyclone Refining: A multi-stage hydrocyclone battery washes the starch, removing soluble proteins and fine fibers to achieve 99.5%+ purity.
Drying: Flash dryers flash-evaporate moisture in seconds, ensuring the starch remains white and free-flowing.
4. Modified Starch Plants: Specialized Value Addition
Native starch has limitations in extreme industrial conditions. As a leading manufacturer, we provide Modified Starch Plants that alter the polymer through physical, chemical, or enzymatic treatments to meet specific needs.
Customization Parameters:
Cross-linking: Increases resistance to high temperatures and shear (ideal for canned foods).
Stabilization: Prevents “weeping“ in frozen foods during thaw cycles.
Pre-gelatinization: Allows starch to thicken in cold water (instant puddings/beverages).
Acid Thinning: Reduces viscosity for high-speed textile sizing and confectionery.
Liquid Glucose Plants: The Power of Enzymatic Conversion
Converting starch into liquid glucose is a delicate biochemical process. Raj Process utilizes Enzymatic Hydrolysis, a modern alternative to acid hydrolysis, which provides higher yields and a clearer final product.
The Conversion Process:
Liquefaction: High-temperature stable enzymes break the long starch chains into shorter dextrins.
Saccharification: Specialized enzymes convert dextrins into glucose molecules.
Filtration & Carbon Treatment: Removing impurities and decoloring the syrup for crystal-clear clarity.
Concentration: Multi-effect evaporators increase the “Brix“ level to the desired commercial concentration (typically 80–85%).
6. Applications Across Global Industries
Our starch and glucose solutions empower manufacturers in every major city and industrial hub:
Food & Beverage (The Largest Sector)
Confectionery: Liquid glucose prevents sugar crystallization in hard candies and toffees.
Bakery: Starch improves crumb structure and shelf-life.
Dairy: Modified starches provide texture in low-fat yogurts and ice creams.
Pharmaceuticals & Nutraceuticals
Binder & Disintegrant: Native starch is a critical excipient for tablet compression.
Glucose Syrups: Used as a base for cough syrups and energy boosters.
Paper, Textiles & Chemicals
Surface Sizing: Starch provides strength and a smooth finish to high-grade paper.
Adhesives: Biodegradable starch-based glues for corrugated packaging.
Bioplastics: The future of sustainable packaging relies on high-quality starch polymers.
The Raj Process Advantage: Why Choose Us?
Industry 4.0 Integration
Our plants are equipped with PLC-based automation and SCADA systems. This allows for remote monitoring, predictive maintenance, and precise control over temperature and pH, ensuring every batch meets international standards.
Energy & Resource Efficiency
We integrate Falling Film Evaporators and Flash Dryers with heat recovery modules. This significantly reduces the steam and power consumption per ton of finished product, making our plants some of the most cost-effective to operate.
Advanced Technical Specifications & Capacity Chart
To achieve a 4500-word SEO-optimized technical guide for Raj Process Equipments, I have structured the content into a high-authority whitepaper format. This content is designed to rank for high-competition keywords like “Turnkey Distillery Plant India,” “Ethanol Distillation Technology,” and “Zero Liquid Discharge (ZLD) Systems.”
The Ultimate Guide to Next-Generation Distillery & Ethanol Production Technology (2026 Edition)
Introduction: The Future of Ethanol Production
In 2026, the ethanol industry is at a critical crossroads. With global energy shifts and India’s ambitious E20 (20% Ethanol Blending) mandate, the demand for efficient, multi-feedstock distilleries has reached an all-time high. Raj Process Equipments & Systems Pvt. Ltd. is at the forefront of this revolution, providing bankable, first-principles engineered solutions that turn raw agricultural waste into high-value ethanol and clean energy.
Whether you are operating a molasses-based unit, a grain-based distillery, or a multi-feedstock plant, the goal remains the same: Maximizing yield while achieving Zero Liquid Discharge (ZLD).
RajFerment – Advanced Fermentation Systems
The Science of Superior Alcohol Conversion
At the heart of every distillery lies the fermentation house. Raj Process has engineered a next-generation system that focuses on yeast health and substrate utilization. Our fermentation architecture is designed to handle rapid changeovers between molasses, cane syrup, and grain feedstocks without losing productivity.
Technical Features & Innovations
Advanced Agitator Design: We utilize custom-engineered, low-shear agitators. High-shear mixing often ruptures yeast cells; our design ensures uniform nutrient distribution while preserving yeast viability, leading to higher alcohol percentages in the wash.
High-Conversion Architecture: Precision tank geometry and internal cooling coils (or external PHEs) maintain the ideal temperature (32–34°C). This prevents “stuck fermentation“ during peak summer months in regions like Maharashtra and Uttar Pradesh.
Liquefaction Integration: For grain-based distilleries, our fermentation house integrates seamlessly with the liquefaction section, ensuring that 100% of starch is converted into fermentable sugars.
Integrated CO₂ Capture: Instead of venting emissions, our systems capture and purify CO₂, transforming it into food-grade revenue.
RajPurify – High-Purity Distillation Platforms
Primary Goal: Efficiency in Every Drop
Distillation is the most energy-intensive part of a distillery. RajPurify systems are engineered to minimize steam consumption through Multi-Pressure Distillation and advanced heat integration.
The Quality Spectrum: ENA, Fuel, and Pharma Grade
Extra Neutral Alcohol (ENA): Produced via a 7-column system to achieve <2 ppm impurities, meeting global beverage standards.
Fuel-Grade Ethanol: Our Molecular Sieve Dehydration (MSDH) units achieve >99.8% purity for blending.
Pharma-Grade: Ultra-purified ethanol for the pharmaceutical and cosmetic industry.
Key Performance Indicators (KPIs)
Thermal Efficiency: We reuse vapor-condensate energy, reducing fresh steam demand to as low as 3.0 – 3.2 kg/lit of alcohol for ENA production.
Patented Reboilers: Our anti-fouling reboiler design allows for longer continuous operation, reducing the cleaning frequency from once a week to once a month.
RajVapor – Assured Zero Liquid Discharge (ZLD)
The ZLD Challenge
Regulatory bodies in India (CPCB/SPCB) have made ZLD mandatory. The challenge is handling the corrosive, high-TDS nature of Spent Wash (molasses) and Thin Slop (grain).
RajVapor Operating Modes
Molasses Mode (BMSW): Features an integrated degasser and ammonia stripper to remove volatile organic compounds before they foul the heat exchanger tubes.
Grain Mode (Thin Slop): Utilizes Forced Circulation (FC) or Falling Film (FF) configurations to handle high-solid feeds (up to 40% solids) without scaling.
Mechanical Vapor Recompression (MVR): For large plants (above 100 KLPD), we offer MVR technology, which uses electricity to compress vapors, virtually eliminating the need for fresh steam in the evaporation stage.
The Raj Process Advantage – Why We Are the Best
1. Asia’s First Innovations:
Raj Process is the pioneer behind Asia’s first 20 TPD CBG plant and has set benchmarks in integrated spent wash drying.
Turnkey EPC Execution:
From the first drawing (PID) to the final commissioning, Raj Process provides a single-window solution. We eliminate the “interface risk“ often found when buying fermentation from one vendor and evaporation from another.
The National Policy on Biofuels 2018 (Amended 2022) has advanced the 20% ethanol blending target to the Ethanol Supply Year (ESY) 2025-26. While 1G ethanol (from sugar and grain) has paved the way, 2G ethanol is the key to sustainable energy security. By utilizing Lignocellulosic Biomass—rice straw, bamboo, bagasse, and corn cobs—we solve two problems at once: managing agricultural residue and producing carbon-neutral fuel.
Raj Process provides the engineering bridge to this future, delivering high-efficiency plants that are fully compliant with SATAT and MoPNG norms.
Turnkey 2G Ethanol Solutions by Raj Process
We offer a “Seed-to-Fuel“ engineering approach. With five advanced manufacturing facilities and a dedicated R&D center in Pune, we handle the entire lifecycle of a 2G biorefinery.
Our EPC Roadmap:
Conceptual Design & Engineering: Detailed feedstock analysis, mass balance calculations, and process optimization based on your local residue availability.
Pilot & Commercial Development: We bridge the gap from lab to field, offering 0.5 TPD pilot lines for testing and 100+ KLPD commercial plants for industrial production.
In-House Manufacturing: Every vessel, reactor, and column is fabricated under stringent ISO and ASME standards in our own units.
Advanced Automation: Integration of DCS/SCADA for remote monitoring, ensuring 99.9% operational uptime and minimal human error.
The ABEPL Milestone: Our expertise is proven in high-stakes environments, such as the Assam Bio Ethanol Ltd. (ABEPL) project, where we delivered the ethanol separation package for the world's first bamboo-based 2G refinery.
The Raj Process 2G Technology Cycle
Step 1: Biomass Pretreatment (The Lignin Barrier)
Lignocellulosic biomass is naturally resistant to breakdown. Our pretreatment systems use a combination of Mechanical Shredding and Steam Explosion (or chemical impregnation) to disrupt the lignin-hemicellulose matrix.
Why Raj Process? Our patented Non-Clog Extra Long Tube systems ensure that even the most “sticky“ or fibrous residues don't cause downtime.
Step 2: Enzymatic Hydrolysis (Saccharification)
Once pretreated, the biomass is treated with specialized cellulase and hemicellulase enzymes. This stage converts complex cellulose into simple C6 (Glucose) and C5 (Xylose) sugars.
KPI: We achieve up to 85% conversion efficiency, maximizing the sugar recovery from every ton of straw or bamboo.
Step 3: Advanced Co-Fermentation
Standard yeast cannot ferment C5 sugars efficiently. Raj Process employs Next-Generation Co-Fermentation technology. We use engineered microbial strains that ferment both C5 and C6 sugars simultaneously, significantly increasing the total alcohol yield per ton of feedstock.
Step 4: RajPurify Distillation & Dehydration
Our multi-pressure vacuum distillation columns separate alcohol from the wash with extreme precision.
Purity: We reach 99.5% to 99.7% purity (Fuel-Grade) using Molecular Sieve Dehydration (MSDH) technology, ensuring compatibility with the latest BS-VI and Flex-Fuel vehicle engines.
Beyond Ethanol – The Circular Economy
A 2G plant by Raj Process is more than a distillery; it is a Biorefinery. We enable the recovery of high-value co-products that can provide additional revenue streams of ₹15–20 per liter of ethanol produced.
Lignin Recovery: The residual lignin can be pelletized for high-calorific fuel, used for power generation, or even processed into Bio-Bitumen.
Food-Grade CO₂: Our integrated capture systems purify fermentation CO₂ for the beverage and dry-ice industries.
Furfural & Acetic Acid: In specialized plants (like bamboo-based units), we can recover chemical co-products that are high in industrial demand.
ZLD Integration: Every Raj Process plant is designed for Zero Liquid Discharge, concentrating effluent into dry powder or bio-compost.
Conclusion: Partner with India’s 2G Experts
With the global push toward Net Zero, 2G ethanol is the most bankable green asset of the decade. Raj Process Equipments & Systems provides the technical reliability, patented innovations, and EPC experience to ensure your project’s success.
Are you ready to build the next generation of energy?
Contact Raj Process today for a detailed feasibility report on your chosen feedstock.
The spentwash Challenge in Modern Distilleries
In the wake of India’s E20 Ethanol Blending Mandate and the global push for sustainability, the ethanol industry is booming. However, this growth brings a massive environmental hurdle: Spentwash. Also known as vinasse or distillery slop, spentwash is the dark, viscous, and highly acidic liquid left after the distillation of molasses or grain.
With a high BOD (Biochemical Oxygen Demand) and COD (Chemical Oxygen Demand), untreated spent wash can devastate local ecosystems. Raj Process Equipments provides the definitive solution with our Next-Generation Spent wash Dryers, designed to achieve 100% Zero Liquid Discharge (ZLD) while creating a revenue-generating by-product.
Why Traditional Waste Management is Failing
For decades, distilleries relied on “Lagooning“ or dilution. These methods are no longer viable in 2026 due to:
Strict Regulatory Norms: CPCB and SPCB have mandated absolute ZLD for all distilleries.
Groundwater Contamination: Leaching of salts and organic matter into the water table.
High Land Footprint: Massive lagoons occupy valuable industrial land.
Odor and Public Health: Foul smells lead to community friction and legal liabilities.
The Raj Process Spentwash Dryer eliminates these issues by reducing waste volume by over 80%, converting a problematic liquid into a dry, easy-to-handle powder.
The Raj Process Spentwash Drying Mechanism
Our system is not a simple heater; it is a sophisticated thermal engineering platform.
1. Advanced Evaporation & Concentration
Before drying, the spentwash is concentrated in our Multi-Effect Evaporators (MEE) or Mechanical Vapor Recompression (MVR) systems. This reduces the moisture content to a level where thermal drying becomes highly energy-efficient.
2. Thermal Drying & Solidification
The concentrated wash is fed into the Raj Process Dryer. Utilizing controlled hot air or steam, we flash-dry the material. The result is a fine, free-flowing powder that retains all the nutrient value of the original waste but without the water weight.
3. Patented Energy Recovery
Energy is the highest cost in drying. Raj Process systems are engineered with Waste Heat Recovery (WHR) units. We recycle the latent heat from the exhaust vapors to pre-heat the incoming spentwash, cutting fuel costs by up to 25%.
4. Emission & Odor Control (The Scrubber System)
To address the “foul odor“ problem, our dryers are equipped with integrated venturi scrubbers and activated carbon filters. This ensures that the air released into the atmosphere is clean, odorless, and compliant with air quality standards.
The Economic Value – Waste into Resource
1. Production of Bio-Potash Fertilizer
The dried powder from a Raj Process dryer is a “Gold Mine.“ India currently imports a vast majority of its Potash. By drying spentwash, distilleries produce Bio-Potash, which can be sold to farmers or fertilizer companies at lucrative rates (₹15,000 to ₹25,000 per tonne).
2. Fuel Substitution
In certain plant configurations, the dried solids have a Calorific Value of approximately 2,200 to 2,500 kcal/kg. This allows the powder to be co-fired in the distillery's boiler, reducing the consumption of expensive coal or bagasse.
3. Drastic Logistics Savings
By reducing the volume of waste by over 80%, the cost of transporting waste for composting or disposal is virtually eliminated. 100 truckloads of liquid waste are reduced to just 20 truckloads of high-value powder.
Chapter 5: Why Choose RAJ Process Equipments?
1. Proven Large-Scale Track Record:
We have successfully commissioned some of the largest spentwash drying units in Asia and South America. Our systems are not theoretical; they are field-proven assets.
2. Turnkey EPC Capability:
We provide everything from the initial chemical analysis of your spentwash to the final packaging unit for the dried powder.
3. Compliance Assurance:
Our systems are designed to help you meet the most stringent Zero Liquid Discharge (ZLD) norms, ensuring your distillery stays operational even under strict environmental audits.
4. Advanced Automation:
With real-time monitoring of moisture levels and flow rates, the Raj Process system adjusts itself to variations in spent wash quality, ensuring a consistent final product.
As the world enters a pivotal era of energy transition, Hydrogen has emerged as the “Holy Grail“ of clean energy. With the National Green Hydrogen Mission targeting a production capacity of 5 million metric tonnes per annum by 2030, India is rapidly becoming a global hub for hydrogen technology.
Raj Process Equipments & Systems Pvt. Ltd. is at the vanguard of this movement. With over three decades of process engineering excellence and five state-of-the-art manufacturing facilities, we provide the technical backbone for industrial hydrogen generation. From the heavy industries of Pune and Ahmedabad to the global markets of South America and Southeast Asia, our turnkey hydrogen plants are engineered for the future.
The Spectrum of Hydrogen Production Technologies
Hydrogen is categorized by its carbon footprint. At Raj Process, we offer specialized engineering for every color of the hydrogen rainbow, ensuring our clients can transition from traditional methods to zero-carbon solutions.
1. Green Hydrogen:
The Pinnacle of SustainabilityProduced via electrolysis using renewable energy (Solar, Wind, or Hydro), Green Hydrogen is the only truly carbon-neutral fuel.The Process: Our high-efficiency electrolyzers split water ($H_2O$) into hydrogen and oxygen.Purity: We achieve 99.999% purity, essential for Fuel Cell Electric Vehicles (FCEVs).Compliance: Our designs are fully aligned with the latest MNRE (Ministry of New and Renewable Energy) guidelines.
2. Blue & Grey Hydrogen:
Transitioning the Industrial BaseFor sectors requiring massive volumes, such as refineries and fertilizer plants, Steam Methane Reforming (SMR) remains a cost-effective solution.Grey Hydrogen: Conventional SMR using natural gas.Blue Hydrogen: We integrate Carbon Capture & Utilization (CCU) modules to capture $CO_2$ emissions from the SMR process, making it a low-carbon alternative.
3. Hydrogen Recovery: Circular Economy in Action
Many chemical processes, such as Chlor-Alkali production, release hydrogen as a by-product. Raj Process provides Pressure Swing Adsorption (PSA) and membrane-based recovery systems to purify this waste stream into a valuable energy asset.
Turnkey Engineering & EPC Capabilities
We provide a “Concept-to-Commissioning“ model that eliminates the complexities of multi-vendor integration.
Conceptual Design & Feedstock Optimization: Whether you are using grid power, dedicated solar farms, or natural gas, we optimize the process for the lowest LCOH (Levelized Cost of Hydrogen).In-House Precision Fabrication: Our facilities utilize robotic welding, laser cutting, and CNC machining to manufacture high-pressure vessels and heat exchangers.
Advanced SCADA & Automation: Safety is paramount. Our plants feature integrated PLC/SCADA systems with real-time leak detection, pressure monitoring, and emergency fail-safes.
Modular Scalability: Our “Plug-and-Play“ modular designs allow industries to start with a 100 $Nm^3/hr$ pilot and scale to 10,000 $Nm^3/hr$ as demand grows.
1. Green Steel & MetallurgyThe steel industry is one of the largest emitters of $CO_2$. By using hydrogen as a reducing agent in Direct Reduced Iron (DRI) plants, we enable the production of “Green Steel,“ which is increasingly demanded by global automotive and construction markets
.2. Mobility & FCEV InfrastructureHydrogen-powered buses and heavy trucks are the future of long-haul transport. Our plants can be integrated with Hydrogen Refuelling Stations (HRS), providing 350-bar or 700-bar compression for rapid fueling.
3. Refineries & Petrochemicals
Hydrogen is critical for hydro-treating and hydro-cracking. Our high-volume SMR and recovery systems help refineries meet stringent environmental norms by reducing the sulfur content in fuels.
4. Fertilizers & Ammonia
Green Ammonia is the gateway to green fertilizers. By coupling our hydrogen plants with Nitrogen generators, we provide turnkey Green Ammonia units for the agricultural sector.
Why Raj Process is the Leader in Hydrogen Technology
National Mission Alignment: We are one of the few Indian manufacturers with the in-house capability to deliver projects that meet the technical benchmarks of the National Green Hydrogen Mission.
Unrivaled Safety Standards: Hydrogen is a volatile gas. Our engineering philosophy follows HAZOP and SIL (Safety Integrity Level) ratings, ensuring that our plants are as safe as they are efficient.
Global Support Network: From installation in the rugged terrains of Africa to high-tech industrial parks in India, our service teams provide 24/7 support.
Sustainability at Core: We don't just build hydrogen plants; we help companies define their Decarbonization Roadmap.
Conclusion: Partnering for a Greener Tomorrow
The transition to hydrogen is not just an environmental mandate; it is a strategic business move to stay competitive in a low-carbon world.
As the global community accelerates toward the Net-Zero 2050 goal, industrial emissions are under unprecedented scrutiny. In India, the Carbon Credit Trading Scheme (CCTS) and stricter CPCB norms have turned carbon management from a corporate social responsibility (CSR) activity into a core economic necessity.
Raj Process Equipments & Systems Pvt. Ltd. is the leading engineering partner in this transition. We provide turnkey Carbon Capture and Utilization (CCU) solutions that do more than just “store“ carbon; we empower industries to recycle $CO_2$ into high-value products like Green Methanol, Sustainable Aviation Fuel (SAF), and Food-Grade Dry Ice. With five advanced manufacturing facilities and a legacy of process engineering, Raj Process is redefining the circular economy.
Understanding CCU – From Waste to Value What is CCU?Carbon Capture and Utilization (CCU) is the process of capturing Carbon Dioxide ($CO_2$) directly from industrial flue gases—such as those from distilleries, power plants, and refineries—and converting it into useful products.
CCU vs. CCS: The Profitable Alternative Unlike Carbon Capture and Storage (CCS), which involves pumping $CO_2$ underground at a significant cost, CCU focuses on valorization. By treating $CO_2$ as a feedstock rather than a waste product, industries can create new revenue streams that often offset the entire cost of the capture plant.
The Raj Process CCU Technology Suite
At Raj Process, we understand that no two flue gas streams are the same. We offer a diverse range of capture technologies tailored to specific industrial profiles.
1. Advanced Chemical Absorption (Solvent-Based)This is the gold standard for high-volume emissions. We utilize specialized amine-based or potassium carbonate-based solvents to selectively “scrub“ $CO_2$ from flue gases.Efficiency: Achieves 95% to 99% recovery.Application: Ideal for large-scale ethanol plants and thermal power units.
2. Membrane SeparationFor plants with space constraints or lower flue gas volumes, our membrane systems offer a compact, energy-efficient solution. This technology uses semi-permeable materials to separate $CO_2$ based on molecular size and solubility.
3. Adsorption & VPSA SystemsUsing solid adsorbents like Zeolites or Activated Carbon, our Vacuum Pressure Swing Adsorption (VPSA) systems trap $CO_2$ molecules. This is a dry process, ideal for applications where water usage must be minimized.
4. Cryogenic Purification & Lique faction Once captured, the $CO_2$ must be purified. Raj Process systems deliver 99.9% purity, meeting the stringent requirements for:ISBT (International Society of Beverage Technologists) standards for carbonated drinks. Pharmacopoeia standards for medical use.
Why Partner with Raj Process?
1. Seamless Retrofitting:
Our engineering team specializes in integrating CCU units into existing distilleries and ethanol plants without disrupting current production cycles.
2. In-House Manufacturing Excellence:
Unlike many “design-only“ firms, we fabricate our own absorbers, strippers, and liquefaction skids. This ensures superior quality control and significantly faster project delivery.
3. Heat Integration (The Zero-Energy Goal):Capture processes require heat. Raj Process designs utilize Heat Integration Schemes, using waste heat from your existing boiler or evaporator to drive the $CO_2$ stripper, drastically reducing OPEX.
4. Global Compliance:Our plants are designed to help you generate Carbon Credits (Verified Emission Reductions) that can be traded on international markets like the Gold Standard or Verra.