Thank you for writing to us. One of our executive will reach back to you through your submitted medium. In case there’s an urgency, feel free to connect over WhatsApp for faster response.
Prefer calling? Dial +9108048032972 (international callers) or 08048032972 (Indian callers).
As the world enters a pivotal era of energy transition, Hydrogen has emerged as the “Holy Grail“ of clean energy. With the National Green Hydrogen Mission targeting a production capacity of 5 million metric tonnes per annum by 2030, India is rapidly becoming a global hub for hydrogen technology.
Raj Process Equipments & Systems Pvt. Ltd. is at the vanguard of this movement. With over three decades of process engineering excellence and five state-of-the-art manufacturing facilities, we provide the technical backbone for industrial hydrogen generation. From the heavy industries of Pune and Ahmedabad to the global markets of South America and Southeast Asia, our turnkey hydrogen plants are engineered for the future.
The Spectrum of Hydrogen Production Technologies
Hydrogen is categorized by its carbon footprint. At Raj Process, we offer specialized engineering for every color of the hydrogen rainbow, ensuring our clients can transition from traditional methods to zero-carbon solutions.
1. Green Hydrogen:
The Pinnacle of SustainabilityProduced via electrolysis using renewable energy (Solar, Wind, or Hydro), Green Hydrogen is the only truly carbon-neutral fuel.The Process: Our high-efficiency electrolyzers split water ($H_2O$) into hydrogen and oxygen.Purity: We achieve 99.999% purity, essential for Fuel Cell Electric Vehicles (FCEVs).Compliance: Our designs are fully aligned with the latest MNRE (Ministry of New and Renewable Energy) guidelines.
2. Blue & Grey Hydrogen:
Transitioning the Industrial BaseFor sectors requiring massive volumes, such as refineries and fertilizer plants, Steam Methane Reforming (SMR) remains a cost-effective solution.Grey Hydrogen: Conventional SMR using natural gas.Blue Hydrogen: We integrate Carbon Capture & Utilization (CCU) modules to capture $CO_2$ emissions from the SMR process, making it a low-carbon alternative.
3. Hydrogen Recovery: Circular Economy in Action
Many chemical processes, such as Chlor-Alkali production, release hydrogen as a by-product. Raj Process provides Pressure Swing Adsorption (PSA) and membrane-based recovery systems to purify this waste stream into a valuable energy asset.
Turnkey Engineering & EPC Capabilities
We provide a “Concept-to-Commissioning“ model that eliminates the complexities of multi-vendor integration.
Conceptual Design & Feedstock Optimization: Whether you are using grid power, dedicated solar farms, or natural gas, we optimize the process for the lowest LCOH (Levelized Cost of Hydrogen).In-House Precision Fabrication: Our facilities utilize robotic welding, laser cutting, and CNC machining to manufacture high-pressure vessels and heat exchangers.
Advanced SCADA & Automation: Safety is paramount. Our plants feature integrated PLC/SCADA systems with real-time leak detection, pressure monitoring, and emergency fail-safes.
Modular Scalability: Our “Plug-and-Play“ modular designs allow industries to start with a 100 $Nm^3/hr$ pilot and scale to 10,000 $Nm^3/hr$ as demand grows.
1. Green Steel & MetallurgyThe steel industry is one of the largest emitters of $CO_2$. By using hydrogen as a reducing agent in Direct Reduced Iron (DRI) plants, we enable the production of “Green Steel,“ which is increasingly demanded by global automotive and construction markets
.2. Mobility & FCEV InfrastructureHydrogen-powered buses and heavy trucks are the future of long-haul transport. Our plants can be integrated with Hydrogen Refuelling Stations (HRS), providing 350-bar or 700-bar compression for rapid fueling.
3. Refineries & Petrochemicals
Hydrogen is critical for hydro-treating and hydro-cracking. Our high-volume SMR and recovery systems help refineries meet stringent environmental norms by reducing the sulfur content in fuels.
4. Fertilizers & Ammonia
Green Ammonia is the gateway to green fertilizers. By coupling our hydrogen plants with Nitrogen generators, we provide turnkey Green Ammonia units for the agricultural sector.
Why Raj Process is the Leader in Hydrogen Technology
National Mission Alignment: We are one of the few Indian manufacturers with the in-house capability to deliver projects that meet the technical benchmarks of the National Green Hydrogen Mission.
Unrivaled Safety Standards: Hydrogen is a volatile gas. Our engineering philosophy follows HAZOP and SIL (Safety Integrity Level) ratings, ensuring that our plants are as safe as they are efficient.
Global Support Network: From installation in the rugged terrains of Africa to high-tech industrial parks in India, our service teams provide 24/7 support.
Sustainability at Core: We don't just build hydrogen plants; we help companies define their Decarbonization Roadmap.
Conclusion: Partnering for a Greener Tomorrow
The transition to hydrogen is not just an environmental mandate; it is a strategic business move to stay competitive in a low-carbon world.
Typical Capacity
10 - 2,000 $Nm^3/hr$ // 500 - 10,000+ $Nm^3/hr$
Purity Level
99.999% // 99.99%
Output Pressure
30 - 35 Bar (Pre-compression) // 15 - 25 Bar
Energy Consumption
4.5 - 5.0 $kWh/Nm^3e // Feedstock Dependent
Carbon Footprint
Zero (with RE) // Low (85-95% Capture)
MOC (Reactor)
Nickel-plated Steel / SS 316L // High-Alloy Reformer Tubes
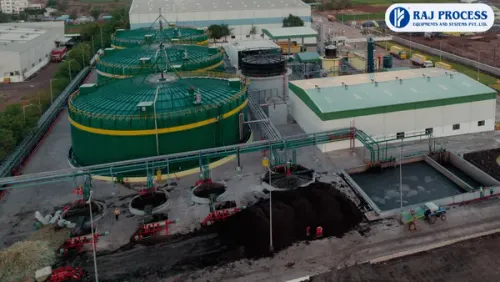
Raj Process Equipments & Systems Pvt. Ltd. is a pioneer in compressed biogas (CBG) technology, offering patented solutions for biogas generation and purification. As one of India’s leading CBG plant manufacturers, we deliver turnkey systems that convert organic waste into high purity compressed biogas — a sustainable, eco friendly fuel for the future.
Aligned with national initiatives like SATAT and GOBARdhan, Raj Process is driving India’s clean energy transition by designing and executing next generation CBG plants across the country and globally.
Organic Waste In. Clean Fuel and Fertilizer Out.
Compressed Biogas — commonly called Bio-CNG — is biomethane produced from the anaerobic digestion of organic waste, purified to 96–99% methane purity, and compressed to 200–250 bar for dispensing and sale. It is chemically identical to fossil CNG in energy value, calorific content, and physical properties. Every CNG vehicle on the road can run on CBG without any modification. Every existing CNG dispensing station is compatible.
The process, in simple terms:
Organic waste enters a sealed, temperature-controlled digester. Over 15–25 days, a carefully managed consortium of microorganisms breaks it down and produces raw biogas — typically 55–65% methane and 35–40% CO₂. This raw biogas passes through our cleaning and upgrading systems, where CO₂, hydrogen sulphide, moisture, and trace contaminants are removed. What remains is biomethane meeting IS 16087:2023 specifications. We compress it, store it in high-pressure cascade systems, and it is ready for sale to Oil Marketing Companies or direct consumers.
The digestate — the solid and liquid material remaining after digestion — is not waste. It is a nutrient-rich Fermented Organic Manure (FOM) and bio-slurry that sells as a premium organic fertilizer, adding a second revenue stream to your plant from day one.
One plant. One waste problem solved. Two revenue streams generated. That is the CBG business model.
FEEDSTOCKS
The feedstock landscape for CBG production in India is broad. We have designed and commissioned plants running on:
Napier grass and dedicated energy crops
Press mud from sugar mills
Cattle and cow dung
Distillery spent wash — molasses based and grain-based
Municipal solid waste (organic fraction)
Poultry litter
Food processing effluents
Fruit and vegetable market waste
Rice straw and wheat straw
Sugarcane trash and bagasse
Sewage sludge
Biogas yields across these feedstocks range from 30 m³ per tonne for cattle dung to 350–400 m³ per tonne for high-fat food waste. The differences are not just in yield — each feedstock brings its own pre-treatment requirements, C:N ratio considerations, sulphur loading, and digester design implications.
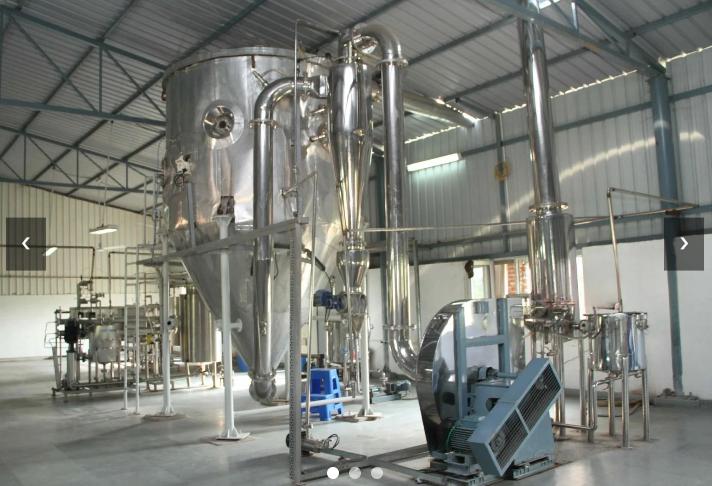
Premium Spray Drying Solutions: Engineering Excellence by Raj Process
In the landscape of industrial thermal processing, Raj Process has solidified its reputation as the premier spray dryer manufacturer in India. Our systems represent the pinnacle of liquid-to-powder conversion technology, offering unparalleled efficiency for diverse industrial sectors.
The Science of Spray Drying: How It Works
Spray drying is a sophisticated method of producing a dry powder from a liquid or slurry by rapidly drying with a hot gas. It is the preferred method for thermally sensitive materials because the drying process is near-instantaneous.
The process follows four fundamental stages:
Atomization: The liquid feed is turned into tiny droplets using a nozzle or rotary atomizer.
Spray-Air Contact: The droplets meet a stream of hot air.
Drying: Moisture evaporates instantly, cooling the particle as it dries.
Separation: The dry powder is recovered from the exhaust air using cyclones or bag filters.
Technical Specifications & Capacity
At Raj Process, we engineer systems that scale with your business. Whether you are in a R&D phase or high-volume industrial production, our equipment is built to perform.
Key Features of Raj Process Spray Dryers
1. Advanced CIP (Cleaning-In-Place) Systems
Hygiene is non-negotiable in pharmaceutical and food processing. Our integrated CIP systems provide:
Automated Cycles: Thorough cleaning without dismantling the machinery.
Cross-Contamination Prevention: Essential for facilities handling multiple product lines.
Reduced Downtime: Faster transitions between product batches.
2. Versatile Feed Handling
Our nozzles and atomizers are designed to handle various feed types:
Solutions: Clear liquids with dissolved solids.
Slurries: Thick, high-viscosity liquids with suspended solids.
Emulsions: Mixtures of immiscible liquids (like oil and water).
3. Precision Control
We utilize advanced PLC-based control systems to monitor inlet/outlet temperatures and feed rates, ensuring a consistent particle size distribution for every batch.
Industrial Applications: Where Precision Meets Scale
As leading manufacturers, we serve a massive spectrum of industries. Below is a detailed breakdown of how our spray dryers are utilized:
Food & Dairy
Milk Powder: Transforming fresh milk into shelf-stable powders while preserving nutritional value.
Fruit Pulps: Creating instant fruit powders for beverages and baking.
Flavors: Encapsulating volatile flavor oils to extend shelf life.
Pharmaceuticals & Biotechnology
Herbal Extracts: Processing sensitive botanicals into concentrated, easy-to-dose powders.
Enzymes: Gentle drying to maintain biological activity.
API Processing: Precise particle engineering for drug delivery.
Chemical & Mineral
Detergents: Large-scale production of uniform, free-flowing washing powders.
Ceramics & China Clay: Preparing fine powders for high-quality molding and glazing.
Dyestuffs: Ensuring consistent color strength and solubility.
Why Choose Raj Process?
Choosing the right spray dryer manufacturer in India is a long-term investment. Raj Process offers:
Custom Engineering: Every system is tailored to the specific thermal sensitivity and viscosity of your product.
Energy Efficiency: Optimized heat recovery systems to reduce operational costs.
Durability: High-grade stainless steel construction (SS316/SS304) for longevity and compliance.
High-Efficiency Rotary Dryer Solutions: The Ultimate Industrial Guide
In the modern industrial landscape, moisture control is the difference between a high-quality product and a wasted batch. As a premier Rotary Dryer Manufacturer, RAJ Process provides engineering marvels designed to handle the most challenging materials with precision, durability, and thermal efficiency.
Our rotary drying systems are engineered to transform wet cakes, powders, and minerals into high-value dry products. Whether you are processing silica sand or delicate coconut powder, our technology ensures uniform drying with minimal energy consumption.
1. What is a Rotary Dryer? (Technical Overview)
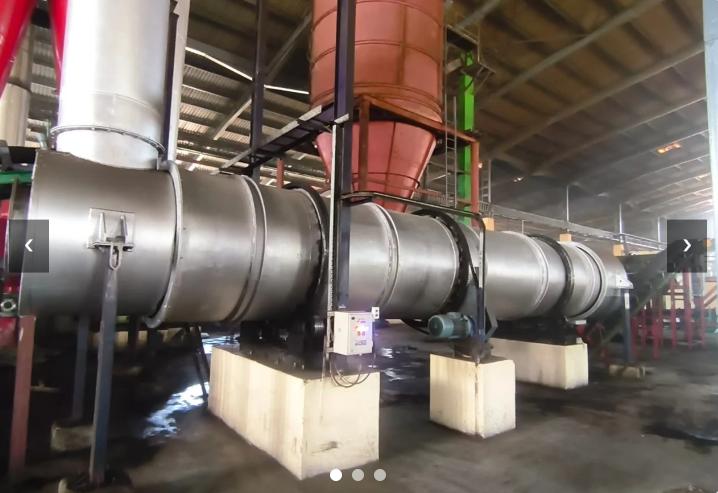
A Rotary Dryer is a type of industrial dryer employed to reduce or minimize the liquid moisture content of the material it is handling by bringing it into direct or indirect contact with a heated gas.
The dryer consists of a large, rotating cylindrical tube, usually supported by steel beams. The dryer slopes slightly so that the discharge end is lower than the material feed end in order to convey the material through the dryer under gravity.
How It Works: The Three-Step Process
Feeding & Distribution: Wet material is fed into the drum. Internal “flights“ (lifting blades) pick up the material and shower it through the hot air stream.
Heat Transfer: As the drum rotates, the material makes contact with heated gas. This can be done via Direct Firing (gas touches material) or Indirect Firing (heat transferred through the drum wall).
Moisture Evacuation: Vaporized moisture is carried away by the air stream and filtered through a cyclone or bag filter, while the dry product exits the lower end.
2. Industry-Leading Capacity & Performance
We design our systems to accommodate everything from boutique processing to massive mining operations.
3. Rotary Dryers vs. Calciners: Versatility Redefined
One of the key advantages of our engineering is the ability to use these units as Calciners.
Drying: Removes surface or bound moisture at lower temperatures.
Calcination: Involves heating the material to high temperatures (up to 600°C) to induce a chemical change or phase transition.
Because our drums are built with heat-resistant alloys, a RAJ Process Rotary Dryer can double as a calciner, making it a “two-in-one“ asset for chemical and mineral plants.
4. Strategic Advantages of Our Rotary Drying Systems
A. Material Versatility
Unlike flash dryers or spray dryers, rotary dryers are incredibly “forgiving.“ They can handle:
Sticky Cakes: Using specialized internal chain systems to prevent clogging.
Non-Uniform Sizes: From fine dust to large mineral chunks.
Abrasive Solids: Reinforced shells that withstand constant friction.
B. Energy Efficiency & Heat Recovery
We integrate advanced heat exchangers that pre-heat the incoming air using the exhaust gas, significantly lowering the “Cost Per Ton“ of dried product.
C. Customized Internal Flights
The “flights“ inside the drum are the secret to efficiency. We customize flight patterns (radial, cruciform, or honeycomb) based on your material’s flow characteristics to ensure a perfect “curtain“ of material for maximum heat exposure.
5. Extensive Industrial Applications
Our rotary dryers are deployed across diverse sectors. Here is how we add value to specific materials:
Mineral & Construction Industry
Silica Sand: Essential for glass and foundry industries. We provide high-temp drying to ensure 0.1% moisture content.
Limestone & Gypsum: High-capacity drying for cement and wallboard production.
China Clay: Precise temperature control to prevent discoloration.
Agriculture & Food Processing
Coconut Powder: Gentle drying at controlled temperatures to preserve natural oils and flavor.
Bagasse: Converting sugar mill waste into high-calorie biofuel by reducing moisture for better combustion.
Grain & Seed: Large-scale moisture reduction for long-term storage.
Chemical & Waste Management
Sludge Drying: Reducing the volume of industrial sludge for cost-effective disposal.
Fertilizers: Creating free-flowing granules that don't cake during packaging.
6. Engineering & Maintenance: Built for Longevity
As a leading manufacturer, we don't just sell equipment; we provide a lifecycle solution.
Precision Alignment: Our technicians use laser alignment for the trunnion rollers to ensure the drum rotates with minimal vibration, extending the life of the bearings.
Sealing Technology: Advanced graphite or mechanical seals prevent dust leakage and maintain thermal vacuum.
Automation: Fully integrated PLC panels allow for remote monitoring of moisture levels and fuel consumption.